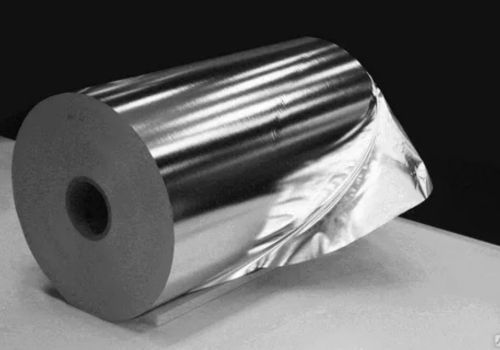
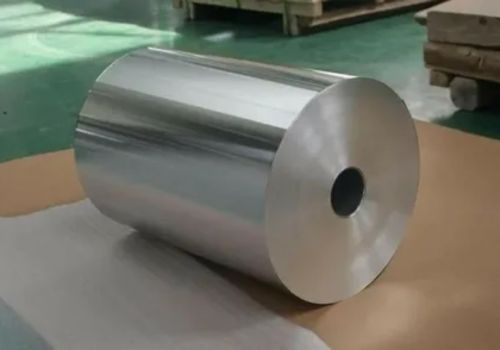
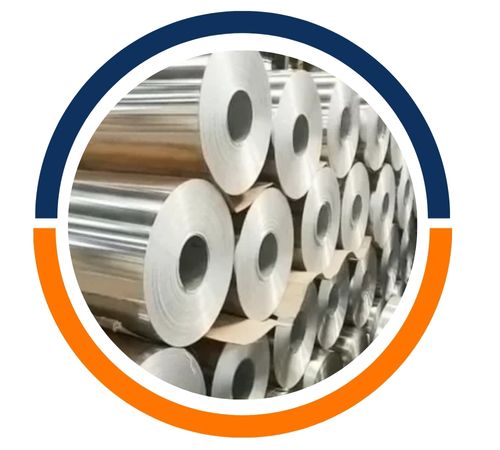
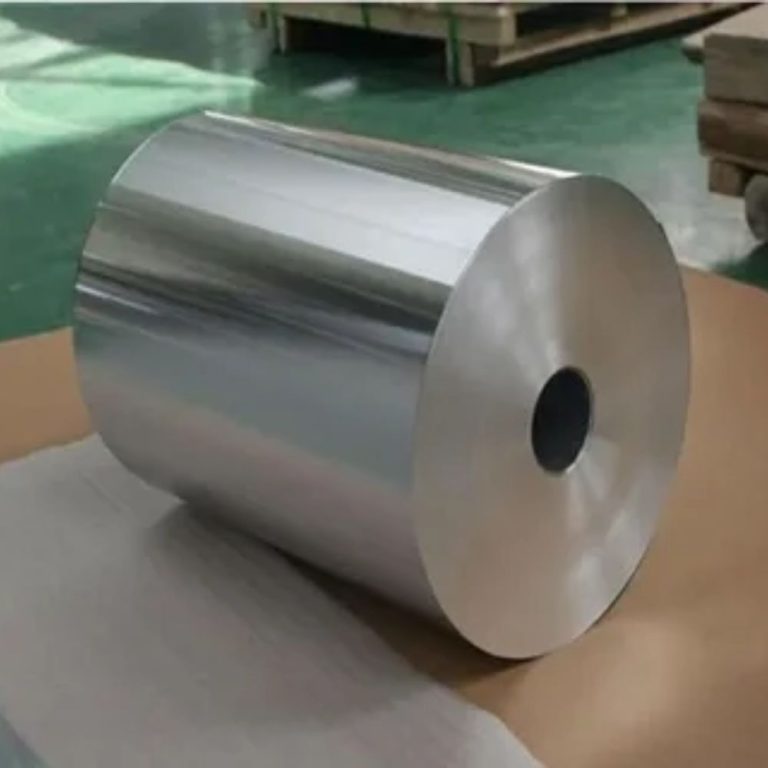
An aluminium foil manufacturer specializes in creating top-notch aluminium foils tailored to meet the diverse needs of packaging, insulation, electrical, and industrial sectors. By utilizing cutting-edge rolling mills and implementing rigorous quality control measures, these manufacturers guarantee a consistent thickness, a superb surface finish, and reliable mechanical properties. Aluminium foils are prized for their lightweight, flexibility, and exceptional ability to block moisture, light, and gases. They come in a variety of grades, thicknesses, widths, and tempers, providing both standard and custom solutions to efficiently cater to the food, pharmaceutical, construction, and industrial markets.
The production of aluminium foil involves high-purity aluminium, where aluminium is the main component and impurities are kept to a minimum. This careful composition ensures excellent resistance to corrosion and great thermal conductivity. On the mechanical side, aluminium foil boasts impressive ductility, decent tensile strength for its thickness, and remarkable formability. It can be easily folded, laminated, coated, or printed on without any risk of cracking. Plus, aluminium foil performs admirably across a wide range of temperatures, making it suitable for both hot and cold uses while keeping its shape and surface quality intact.
Standards : ASTM B479 / ASME SB479
Temper : O,H22,H24
Thickness : 0.018-0.2
Width : Coil/Roll
Length : 100-1600
Surface : Bright, polished, hair line, brush, sand blast, embossed, etching, etc.
Finish :Mill, Customer specific finish
Aluminum Foil Coating : PVC Coated, Color Coated, Polyester, Fluorocarbon, polyurethane and epoxy coating
Type : Hot-Rolled (HR) / Cold-Rolled (CR) Foil
Aluminium foils find their way into various applications, including food and beverage packaging, pharmaceutical blister packs, household wrapping, and container manufacturing. They’re also used in thermal insulation, HVAC systems, cable wrapping, and electrical shielding. Other applications include industrial laminates, heat exchangers, reflective surfaces, and decorative uses. Thanks to their hygienic properties, barrier protection, and recyclability, aluminium foils are perfect for industries that prioritize safety, durability, and sustainability in their packaging and technical applications.
Yes, we offer custom sizes for Aluminium Foils to meet specific project needs. Our team at Himansh Aluminium is committed to providing customized solutions for all your requirements. For more details, contact us at sales@himanshaluminium.com
Aluminium foils are widely used across industries due to their versatility, lightweight nature, and excellent thermal properties. In food packaging, they preserve freshness, prevent contamination, and extend shelf life. In cooking, they are used for baking, grilling, and wrapping food. The pharmaceutical industry relies on aluminium foils for blister packaging to protect medicines from moisture and light. They are also used in insulation for buildings, HVAC systems, and electronics due to their heat-reflective properties. Additionally, aluminium foils serve in automotive, aerospace, and household applications, ensuring durability and efficiency.
Our team is ready to assist you. Contact us for any queries or personalized solutions.
Copyright 2024 Himansh Aluminium. All rights reserved